Advanced Waste Management Solutions: The HICLOVER Waste Incinerator
Introduction to HICLOVER Waste Incinerators
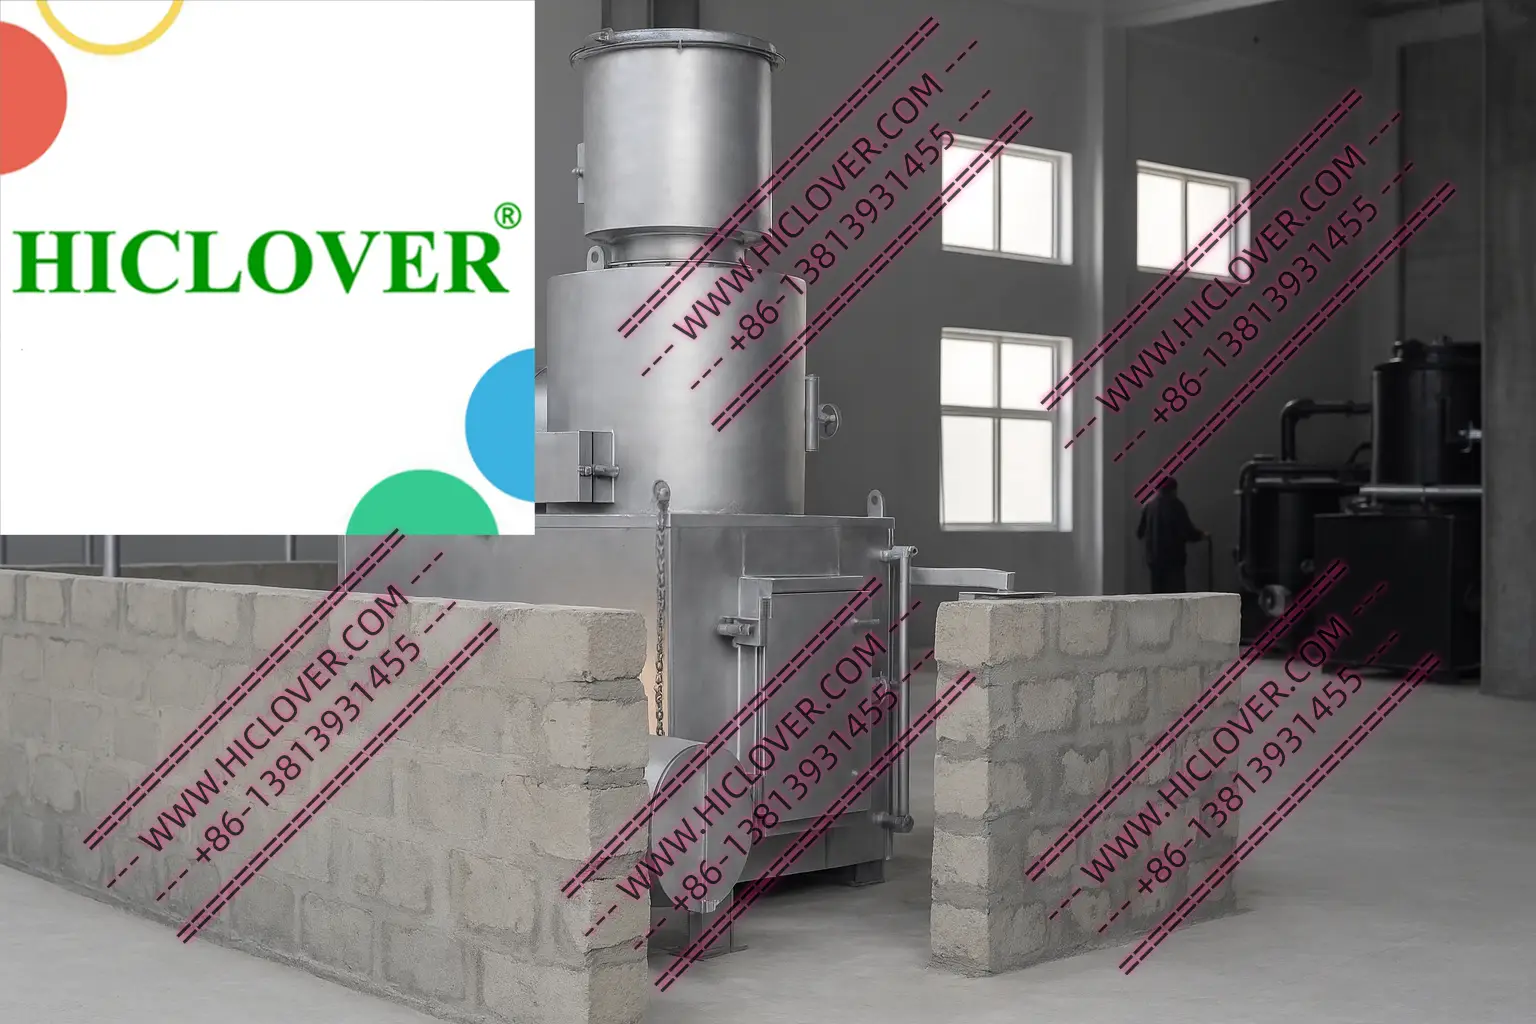
The **HICLOVER waste incinerator** stands as a robust solution for diverse waste disposal needs, particularly in the context of medical waste management and other hazardous materials. Engineered for efficiency, these incinerators comply with stringent **industrial standards** and operate at **high temperatures** ranging from 800°C to over 1200°C, ensuring effective waste degradation. The dual combustion chamber design inherently supports **medical incinerator operating temperature standards**, allowing for comprehensive combustion and minimizing harmful emissions. HICLOVER, as a leading **waste incinerator manufacturer in China**, offers a blend of engineering reliability and advanced technology tailored for today’s environmental challenges.
Technical Specifications and Operational Principles
HICLOVER incinerators employ sophisticated **combustion principles** that align with global regulatory frameworks, including WHO and EU emission standards. The dual chamber system facilitates primary combustion followed by secondary combustion, optimizing the breakdown of complex organic materials. The **high temperature retention** ensures that all waste, including biohazards, undergoes complete thermal destruction, significantly reducing the volume and weight of the residual ash.
The incinerators are designed for **containerized incinerator operation**, making them ideal for deployment in remote locations, such as mining operations or **humanitarian camps**. These units can be customized in size based on specific needs, providing flexibility for varying waste volumes. Furthermore, the integration of **PLC automation** enhances operational efficiency, allowing for precise control and monitoring of the combustion process, which is critical in maintaining compliance with emission norms.
Types of Incinerators and Performance Comparisons
When comparing incinerator types, HICLOVER’s **containerized incinerators** stand out for their modular design, which facilitates easy transport and installation. Unlike fixed installations, these systems can be deployed quickly to crisis zones or **remote oil camps**, ensuring timely waste management solutions.
HICLOVER also offers options between dry and wet scrubbers, addressing different emission control needs. Dry scrubbers are often preferred for their lower operational costs and maintenance, whereas wet scrubbers are effective for higher pollutant load scenarios. The choice between these systems can significantly impact overall operational efficiency and **carbon emission reduction pressure**.
Procurement and Supply Chain Stability
HICLOVER provides factory direct supply, ensuring that clients receive products with consistent quality and engineering expertise. The stability of the supply chain is a critical factor for procurement managers. With **global export capability**, HICLOVER is positioned to meet the diverse requirements of international markets while maintaining compliance with local regulations.
Each incinerator can be tailored, featuring customizable chamber volume options, which allow for **pet animal cremation equipment** to be integrated seamlessly into operations. This customization caters to specific market needs, ensuring that clients find the best fit for their waste management solutions.
Conclusion
Choosing the right waste incinerator involves understanding both technical specifications and operational principles. HICLOVER’s commitment to engineering excellence and resilient supply chains positions its products as a front-runner in the market. For more in-depth technical specifications and to explore models available, visit the [HICLOVER website](www.hiclover.com/). The advanced technology and design of HICLOVER waste incinerators ensure that they meet the challenges of modern waste management, supporting industries in achieving their **ESG compliance** goals while maintaining operational efficiency.